Deliver pasteurised soft drinks with reliablitly, efficiency, and consistent product quality.
In soft drink production, pasteurisation is essential to ensure safety, stability, and shelf life. Achieving consistent quality while maintaining energy efficiency can be a major challenge. Many bottlers and producers face issues such as:
- Temperature fluctuations that put product quality at risk
- Energy-intensive systems with inefficient heat recovery
- Manual control that leads to inconsistent pasteurisation performance
- Product loss due to variable carbonation or flavour degradation
- Difficult maintenance and high downtime from complex or outdated designs
These issues increase costs, reduce yield, and compromise taste and consistency.
Our Solution:
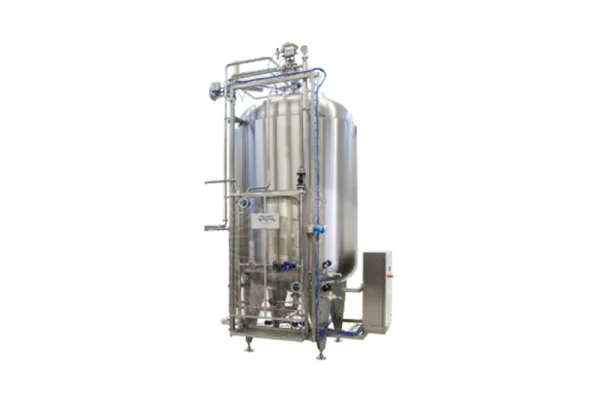
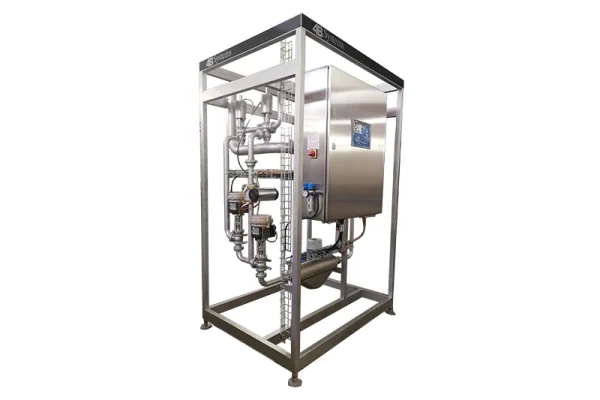
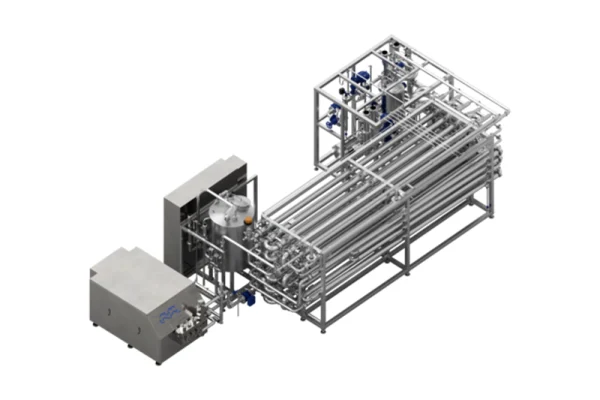
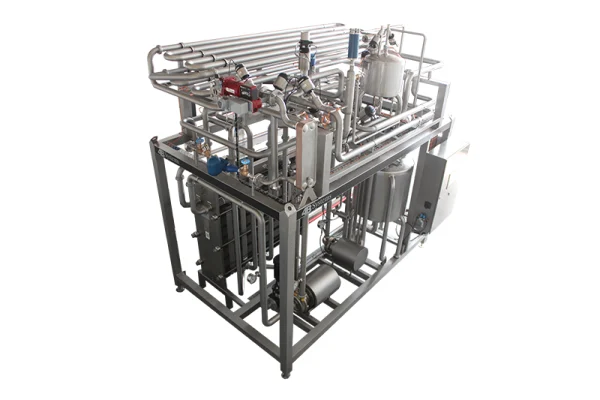
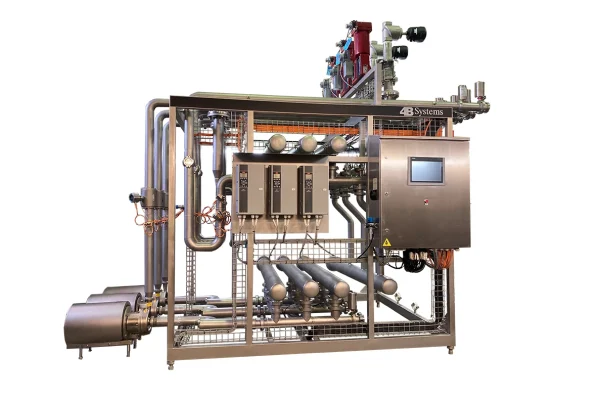
- The 4B Automation & 4B Systems Soft Drink Pasteuriser provides automated, constistant, and energy-efficient pasteurisation for carbonated and non-carbonated beverages.
- Custom-built to your process requirements, it ensures stable product temperature, gentle heat treatment, and minimal energy loss — all while maintaining product flavour, colour, and carbonation.
- With real-time monitoring, remote diagnostics, and full automation, this modular, skid-built system helps you reduce waste, improve consistency, and optimise energy use. Supported locally by 4B Automation & 4B Systems, it’s maintainable, scalable, and designed for long-term reliability.
Key Features / Capabilities
Custom-Built Design:
Tailored to your product type, throughput, and production goals.
Real-Time Monitoring:
Continuous visibility into flow, pressure, and temperature for accurate pasteurisation.
User-Configurable Recipes:
Easily adjust parameters for different soft drink formulations or carbonation levels.
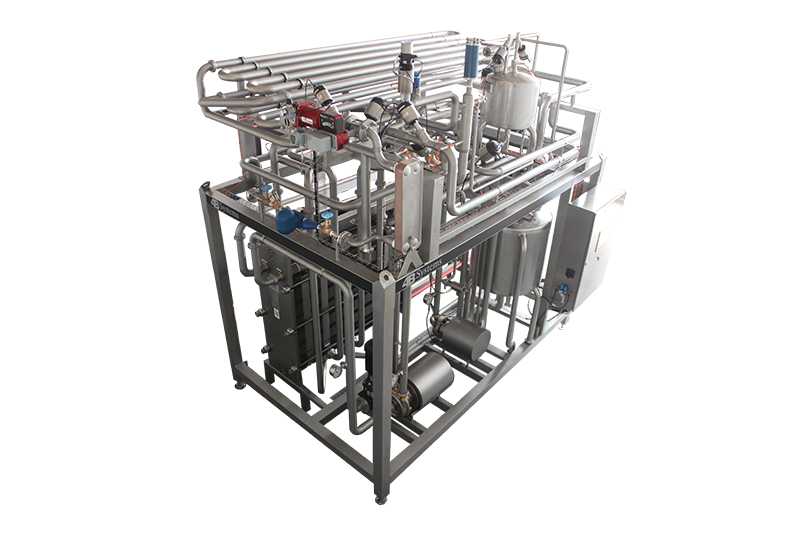
Modular, Skid-Built Design:
Preassembled, compact units for seamless integration into existing lines.
Fully Automated Operation:
Delivers reliable pasteurisation with minimal operator intervention.
Remote Support & Self-Diagnostics:
Enables predictive maintenance, performance alerts, and troubleshooting.
Performance Data & Analytics:
Records critical data for optimisation.
Energy Efficiency & Recovery:
Heat recovery systems reduce energy consumption and operational costs.
High Energy Efficiency:
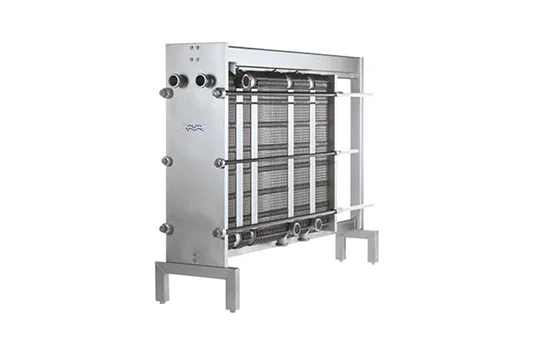
Optimised plate or tubular configurations lower steam and power requirements.
Energy Consumption Monitoring:
Real-time tracking of energy usage for better sustainability.
Product Consistency:
Maintains flavour, carbonation, and colour uniformity across every batch.
Locally Manufactured & Supported:
Built in South African with local spares and engineering support.
Maintainable Design:
Robust, and easy to inspect for long service life.