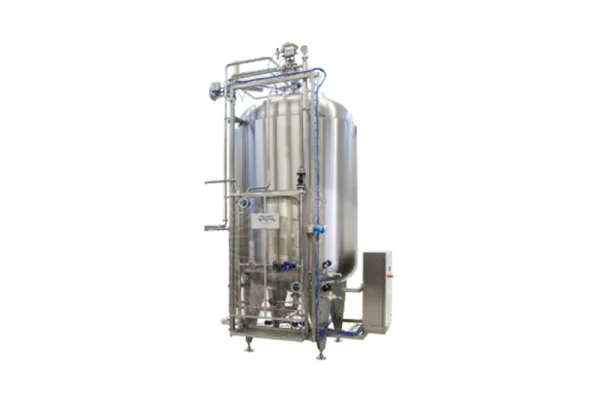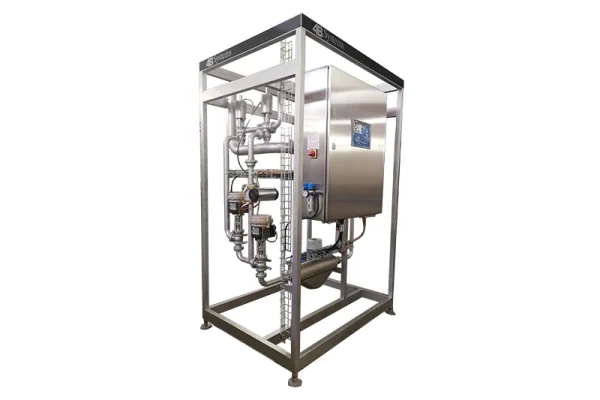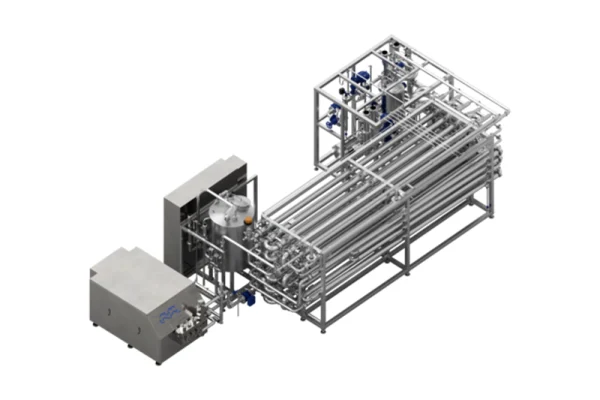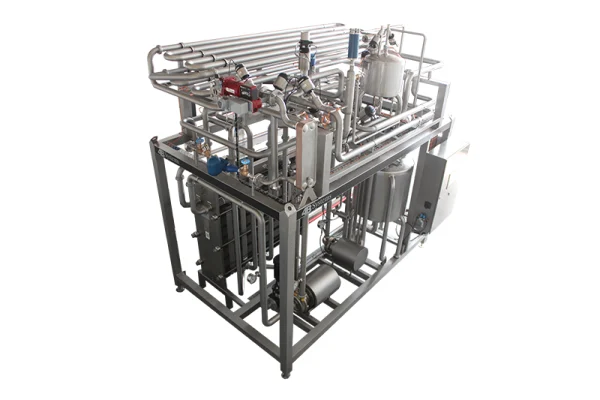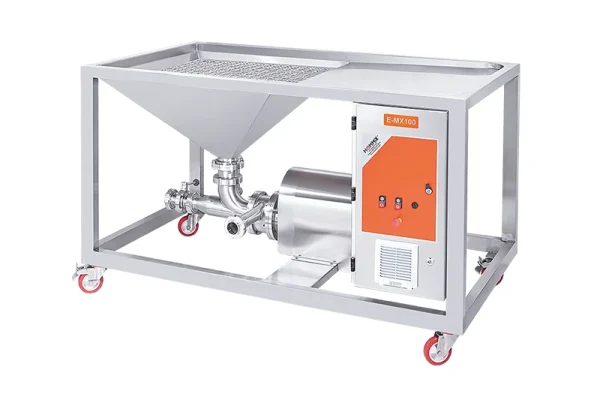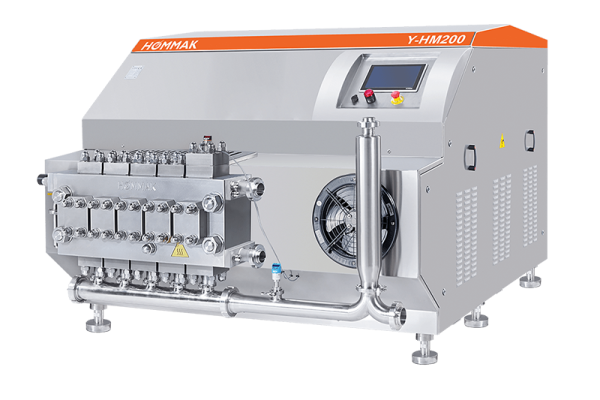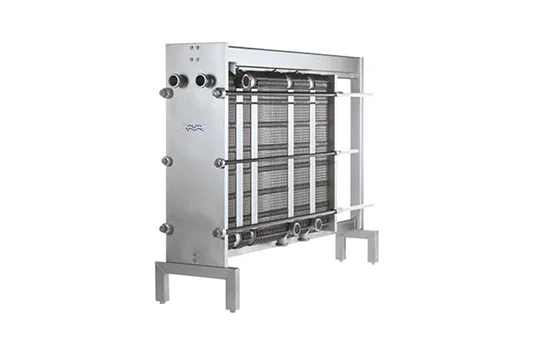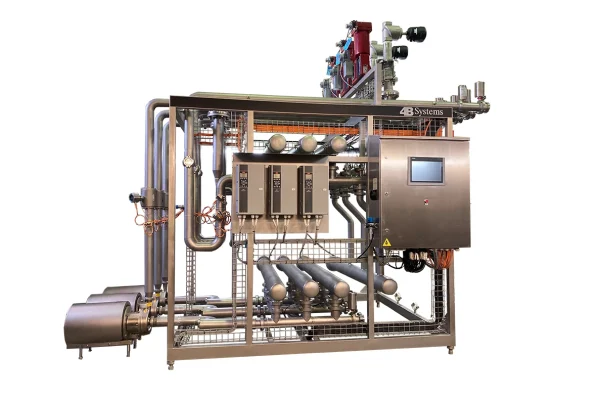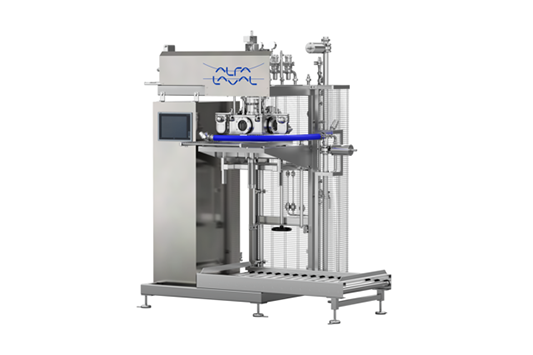
Reliable, energy-efficient sterilisation for soft-drink production; built for consistency and control.
- Soft-drink producers often struggle to maintain consistent sterilisation, control energy costs, and ensure production flexibility.
- Outdated or inefficient sterilisation systems can cause product inconsistencies, higher operating expenses, and reduced throughput, limiting profitability and quality.
Our Solution:
- Our Soft Drink Sterilisers are engineered for precision, consistency, and energy efficiency.
- Equipped with automation, real-time monitoring, and energy-recovery technology, they guarantee superior product safety and quality while optimising performance and energy use.
- Locally manufactured and supported in South Africa, these systems are reliable, maintainable, and scalable, designed to deliver long-term dependability and low total cost of ownership.
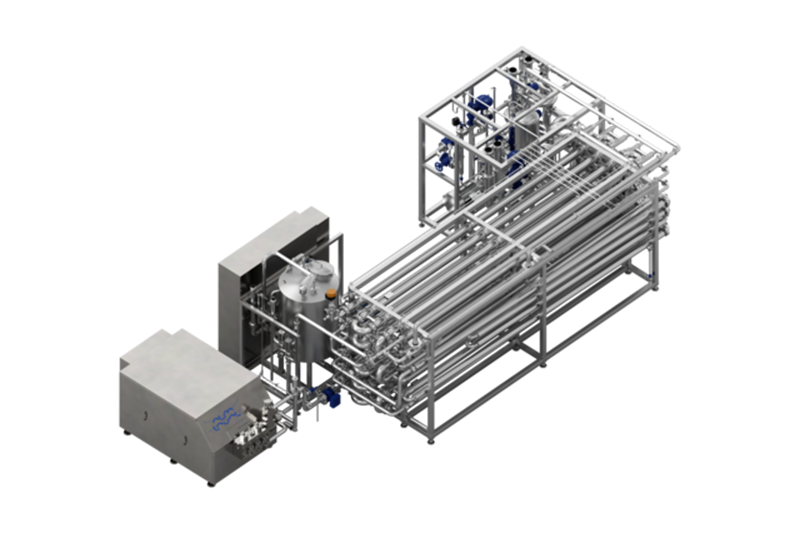
Key Features / Capabilities
Custom-Built:
Designed to meet specific production and product-type requirements.
Real-Time Monitoring:
Continuous visibility of sterilisation data and process variables.
User-Configurable Recipes:
Easily adjust parameters for multiple beverage types.
Modular, Skid-Built Design:
Compact footprint, quick installation, and scalability.
Fully Automated:
Delivers repeatable results with minimal manual input.
Remote Support & Self-Diagnostics:
Rapid troubleshooting and predictive maintenance.
Performance Data & Energy Monitoring:
Track efficiency, recovery, and energy usage.
Energy Efficiency & Recovery:
Energy-recovery systems minimise operating costs.
Product Consistency:
Uniform sterilisation ensures reliable quality batch-to-batch.
Locally Manufactured & Supported:
Accessible parts, service, and expert assistance.
Maintainable:
Built for durability and simple long-term upkeep.