Continuous, reliable solid–liquid separation for higher yield, cleaner product, and efficient processing across multiple industries.
Many processing lines struggle with inefficient separation methods such as settling tanks, filtration, or batch centrifugation. Common challenges include:
- High solids content reducing clarity and quality.
- Yield loss due to inefficient separation.
- Frequent cleaning, fouling, and downtime.
- High energy consumption.
- Inconsistency when feed composition changes.
- Equipment that is hard to integrate, automate, or maintain.
These issues increase operating costs, reduce throughput, and impact product quality; especially in food, beverage, dairy, plant-based, oil, alcohol, and biotechnology applications.
Our Solution:
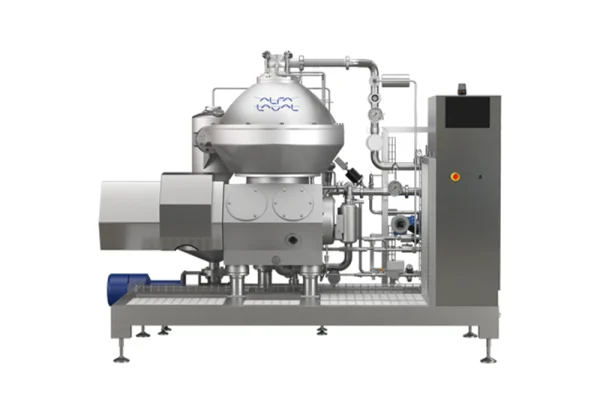
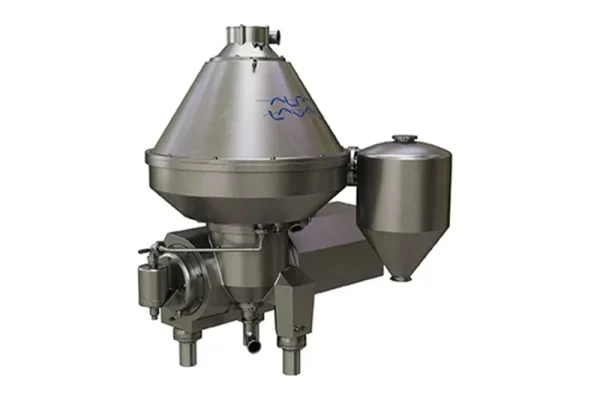
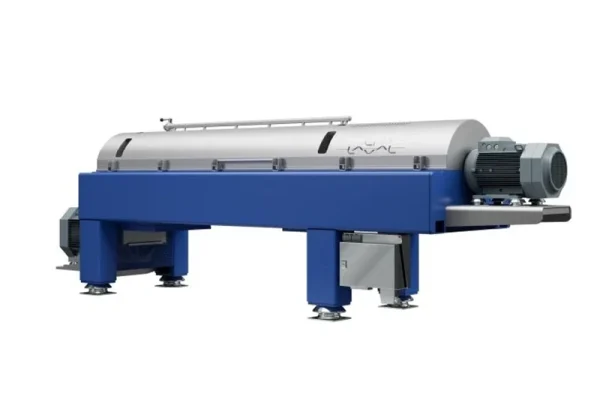
- 4B Automation & 4B Systems supplies, integrates, and supports Alfa Laval Decanters designed for continuous, high-efficiency solid-liquid separation. Built for reliability, hygiene, and energy efficiency, Alfa Laval decanters deliver consistent performance across a wide range of feed types; from dairy and beverages to oils, fruit processing, protein extraction, sugar, biofuel, and biotechnology.
- Each system is configured, automated, and supported locally by 4B Automation & 4B Systems, ensuring seamless operation, easy maintenance, and long-term reliability.
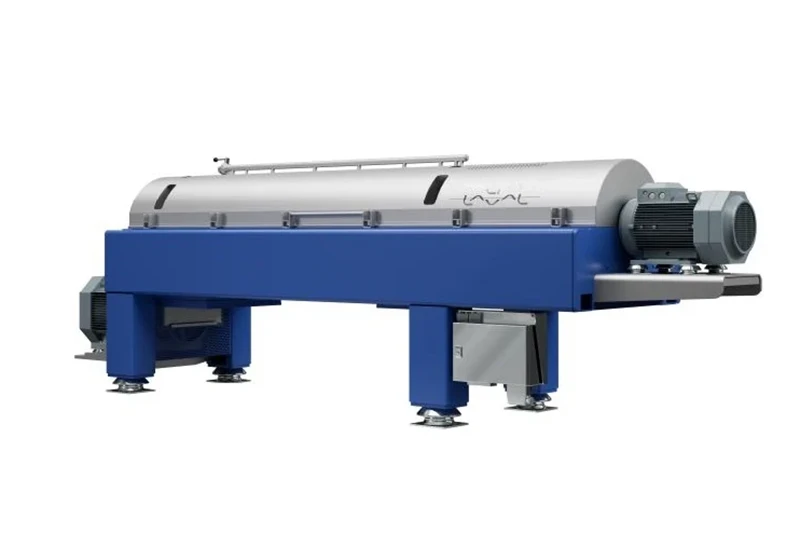
Key Features / Capabilities
Continuous Solid–Liquid Separation:
High-capacity processing with stable, uninterrupted performance.
Handles Wide Feed Variations:
Excels with low- to high-solids streams, fibrous material, viscous slurries, or variable feed conditions.
Adjustable Separation Control:
Fine-tune bowl speed, differential speed, and pond depth for optimal clarity and dryness.
Energy-Efficient Operation:
Optimised bowl geometry, VSD systems, and low-shear feed design minimise power consumption.
Hygienic, Food-Grade Construction:
Stainless-steel contact parts, clean-in-place (CIP) design, and smooth polished surfaces for sanitary operation.
Automation & Real-Time Monitoring:
Integration with process PLCs, recipe control, torque monitoring, and predictive maintenance options.
Robust, Wear-Protected Design:
Engineered for abrasive feeds with wear tiles, protected scrolls, and heavy-duty bearings.
Modular, Skid-Built Layout:
Compact, easy to install, and simple to expand as production grows.
Local Service & Support:
Local support from 4B Automation & 4B Systems, including installation, integration, optimisation, and diagnostics.