Safe, consistent, and energy-efficient sterilisation for premium almond milk production.
Almond milk producers face challenges with maintaining product safety, shelf life, and consistency. Traditional sterilisation systems can be energy-intensive, difficult to control, or inflexible when recipes change; leading to higher costs, inconsistent quality, and operational downtime.
Our Solution:
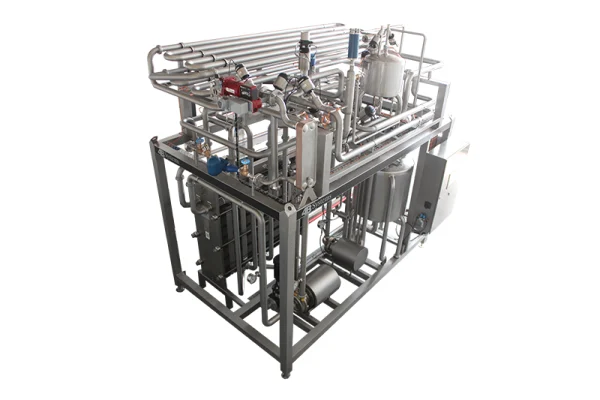
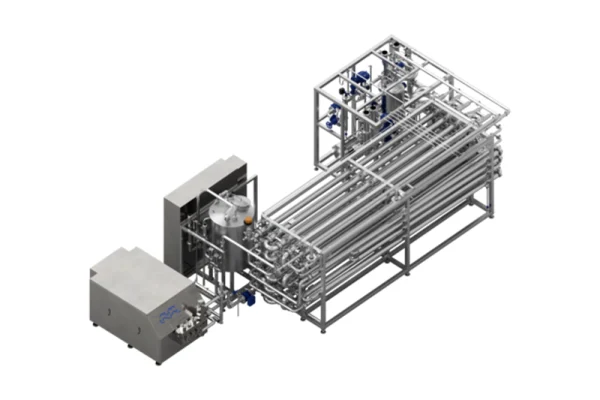
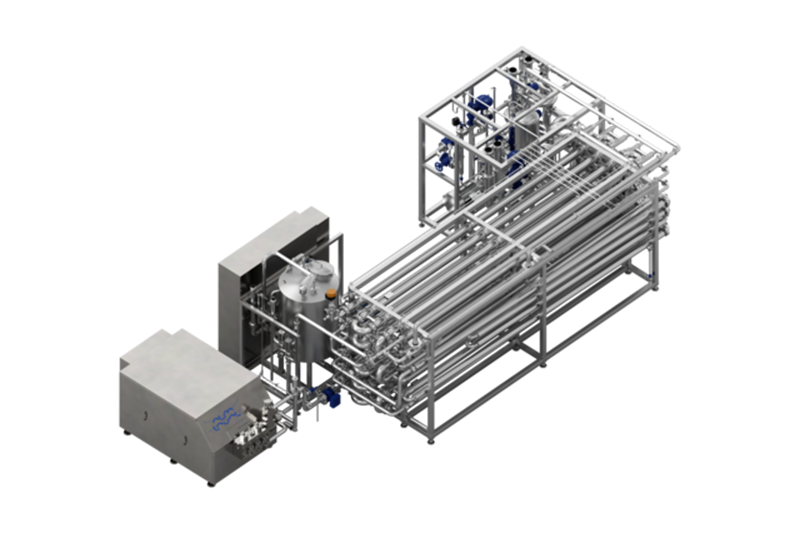
- Our UHT Almond Milk Sterilisers is engineered for consistancy, safety, and efficiency.
- With real-time monitoring, configurable recipes, and energy recovery technology, it delivers consistent sterilisation while optimising energy consumption.
- Locally manufactured and supported in South Africa, its modular skid-based design makes it easy to integrate, maintain, and support; ensuring long-term reliability.
Key Features / Capabilities
Custom-Built:
Designed to meet your unique almond milk processing requirements.
Real-Time Monitoring:
Full visibility of sterilisation performance at every stage.
User Configurable Recipes:
Customise process parameters for different product profiles.
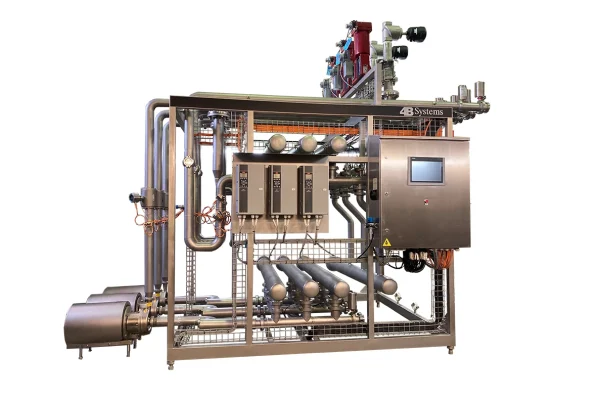
Modular, Skid-Built Design:
Compact, flexible, and plant-friendly layout.
Fully Automated:
Delivers consistent results with minimal manual input.
Remote Support & Self-Diagnostics:
Quick troubleshooting and predictive maintenance.
Performance Data & Energy Monitoring:
Access real-time operational insights.
Energy Efficient & Recovery:
Reduce energy costs through optimised recovery systems.
Consistent Output:
Ensures stable product quality and extended shelf life.
Locally Manufactured & Supported:
Accessible spares, service, and technical expertise.
Maintainable:
Strong, durable construction for reliable long-term operation.